About Industrial Sewage Treatment Plant
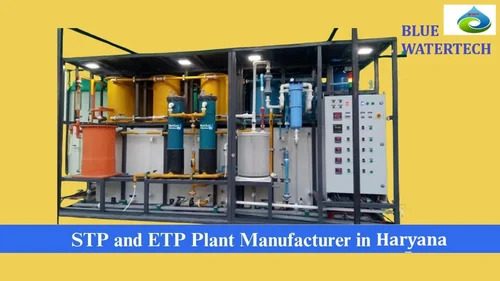
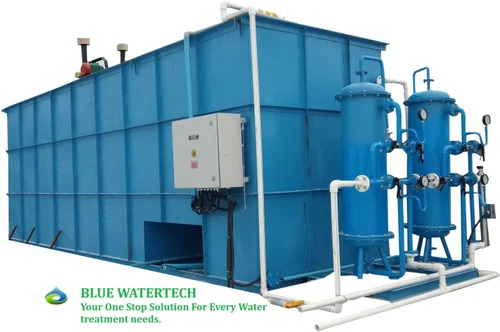
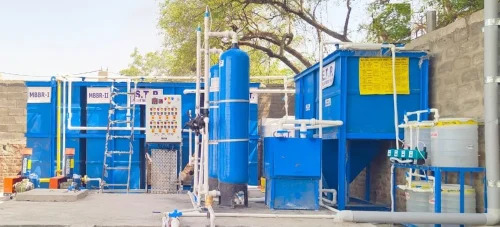
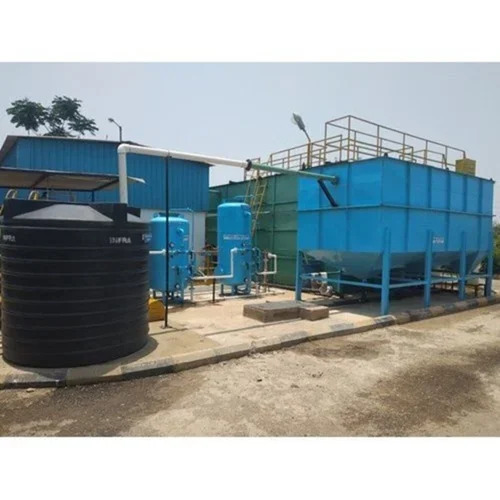
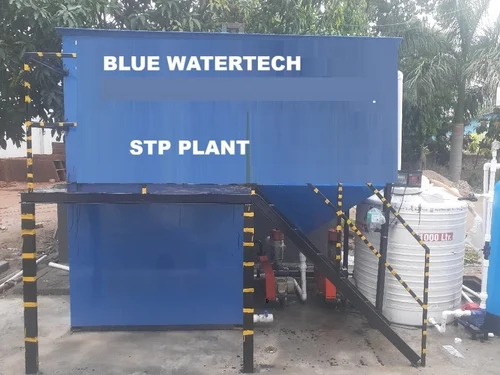
Get the venerable and classic Industrial Sewage Treatment Plant-an absolute must-have for any modern industry prioritizing compliance and efficiency. Engineered with a terrific panel-type electric control system, this packaged STP comes with sturdy MS + FRP lining. Its automatic operation and low noise design ensure smooth and quiet use for both industrial and residential applications. The MBR technology delivers exceptional discharge quality complying with norms. Featuring easy maintenance access, onsite installation, and multicolor appeal, this robust unit supports up to 250 KLD treated water for uses like flushing and cooling towers.
Versatile Application and Area of Use
The Industrial Sewage Treatment Plant is expertly designed for widespread application across industrial estates, factories, and large residential complexes. Suitable for use in manufacturing plants and commercial buildings, its advanced membrane bioreactor technology guarantees effective water treatment. It's ideal for areas demanding reliable, compliant solutions for sewage recycling and reuse. The plant's adaptable structure suits a variety of locations, making it a prudent investment for institutions and industries seeking efficient, space-saving water management solutions.
Logistics and Supply Valuation
FOB Port options include major Indian ports, facilitating smooth international and domestic logistics. Delivery time is swift and reliable, tailored to your project's timeline and site requirements. With significant supply ability, the distributor ensures steady availability and timely dispatch for bulk orders. Comprehensive logistics coordination, competitive valuation, and end-to-end support enable streamlined procurement, installation, and commissioning. Depend on the manufacturer's robust supply chain and prompt service for your industrial sewage treatment needs.
FAQ's of Industrial Sewage Treatment Plant:
Q: How does the Industrial Sewage Treatment Plant work using MBR technology?
A: The plant utilizes advanced Membrane Bioreactor (MBR) technology, combining biological treatment with membrane filtration to produce high-quality treated water that meets regulatory norms for industrial reuse.
Q: What are the primary benefits of using this STP in industrial settings?
A: This STP offers automated operation, easy maintenance access, and a packaged design, ensuring reliable compliance, efficient water recycling, and reduction in environmental footprint for industries.
Q: Where can the treated water from the plant be used?
A: The treated water is suitable for applications such as toilet flushing, cooling towers, and other non-potable uses in industrial and residential projects.
Q: When can I expect delivery after placing an order?
A: Delivery timelines are customized based on the project scope and logistics. Typically, the plant is dispatched within a reasonable lead time after order confirmation and valuation.
Q: What support is available for installation and maintenance?
A: The manufacturer provides onsite installation services, comprehensive instructions, and ongoing support to ensure hassle-free setup and efficient operation. Maintenance is designed to be easy and user-friendly.
 Send Inquiry




 Send Inquiry


 Send Inquiry
